B2B CNC Machine Tool Procurement: Laser Calibration, Factory Acceptance (FAT) & Landed ROI
How industrial buyers verify geometric accuracy before shipment and calculate true 36-month Total Cost of Ownership (TCO) across spindle uptime, tooling compatibility, and ocean logistics.
WMT Metrology & Export Compliance Team
ISO 230-2 Quality Assurance & Global Logistics
Key Engineering Takeaways
- —Never approve ocean shipment without reviewing the machine-specific ISO 230-2 laser interferometry pitch-error compensation chart and dynamic ballbar circularity trace.
- —Specify 3-phase transformer tap matching (220V/380V/400V/440V, 50/60 Hz) and CE/EAC safety interlocks during initial order engineering to eliminate post-arrival electrical retrofits.
- —Container optimization—such as pairing a VMC850 and a TCK50 in a single 40HQ container—reduces landed freight cost per machine by up to 38%.
1. The 4-Stage Factory Acceptance Test (FAT) Protocol
Purchasing a CNC machine tool based solely on catalog brochure specifications exposes production plants to geometric drift and premature ballscrew wear. At WMT Machine, every vertical machining center and CNC lathe undergoes a serialized four-stage verification protocol prior to crating.
First, granite squares and electronic levels verify guideway straightness and spindle-to-table perpendicularity within 0.008 mm/300 mm. Second, a laser interferometer measures bidirectional linear positioning and injects pitch-error compensation tables into the CNC controller. Third, telescopic ballbar testing checks X-Y-Z servo gain balance during circular interpolation. Finally, a continuous 48-hour dry run and test-piece cutting audit confirm thermal equilibrium and zero hydraulic or coolant seepage.
| Verification Stage | Metrology Instrument | WMT Acceptance Tolerance |
|---|---|---|
| Linear Positioning Accuracy | Laser Interferometer (ISO 230-2) | ±0.005 mm (VMC) / ±0.006 mm (TCK) |
| Bidirectional Repeatability | Laser Interferometer | ±0.003 mm across full travel |
| Dynamic Circularity (XY Plane) | Telescopic Ballbar System | ≤ 0.008 mm at 1,000 mm/min feed |
| Spindle Taper Runout | Precision Test Mandrel (300 mm) | ≤ 0.002 mm at spindle nose |
| Continuous Thermal Burn-In | IR Thermal Sensor & Vibration Probe | 48 Hours continuous cycle, ΔT ≤ 18°C |
2. Calculating True 36-Month Landed Cost & Container Logistics
Total Cost of Ownership (TCO) extends far beyond FOB machine price. Smart engineering directors evaluate spindle bearing life, standardized tooling interfaces (BT40 / BMT / VDI), and ocean container utilization.
All WMT machines are treated with VCI anti-corrosion film, vacuum moisture barriers, and heavy structural steel skids engineered for 20GP or 40HQ sea containers—ensuring plug-and-play commissioning within 48 hours of rigging onto your shop floor.
- —Request custom test-cutting video verification on your actual workpiece CAD drawing before final balance release.
- —Standardize controller platforms (FANUC 0i-TF Plus / 0i-MF Plus or Siemens 828D) across your shop to unify post-processors and operator training.
Related Machine Models
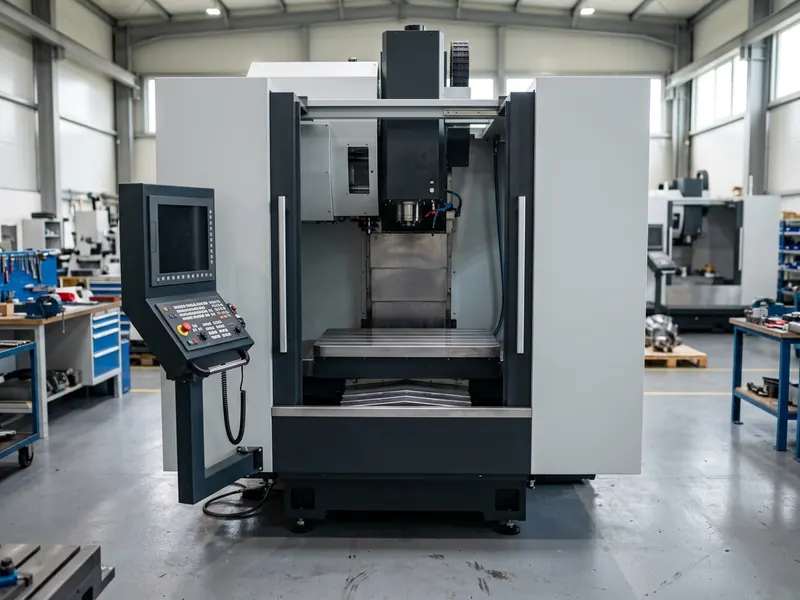
VMC850 Flagship 3-Axis Vertical Machining Center
The global industry benchmark for multi-purpose precision milling, mold cavities, and high-volume job-shop production.
- Travel / Max Swing
- 850 × 500 × 540 mm
- Spindle Speed & Nose
- BT40 · 8,000 / 12,000 RPM
- Main Motor
- 11 / 15 kW
- Repeatability
- ±0.003 mm
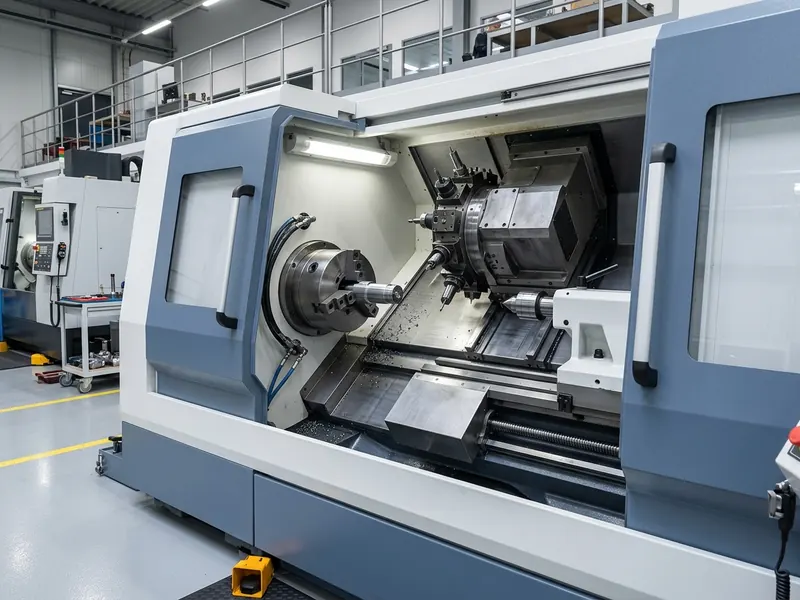
TCK52 Big-Bore 45° Slant Bed CNC Turning Center
Upgraded Ø65 mm through-spindle bar capacity and 550 mm turning length for automated bar feeding and heavy chucking work.
- Travel / Max Swing
- Ø520 mm Swing · 550 mm Length
- Spindle Speed & Nose
- A2-6 · 3,500 RPM · Ø65 mm Bore
- Main Motor
- 11 / 15 kW
- Repeatability
- ±0.003 mm
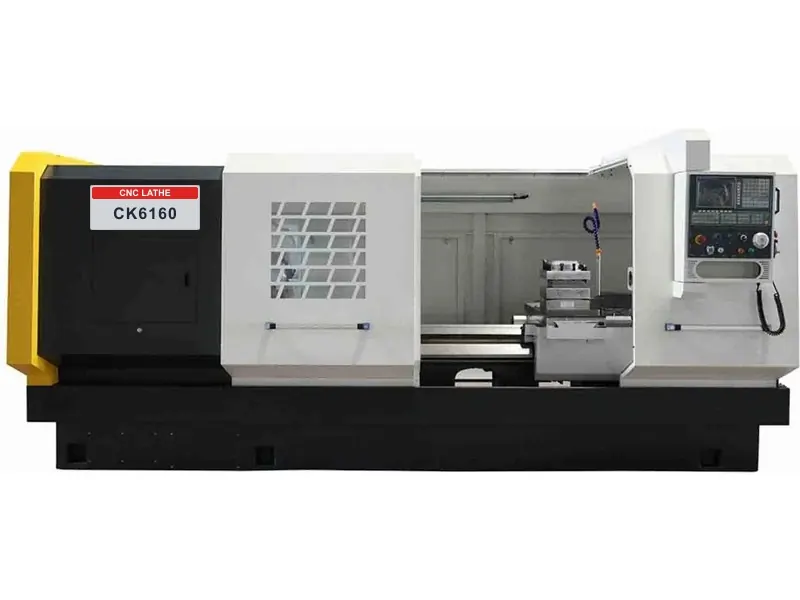
CK6160 Large-Swing Heavy-Duty Horizontal CNC Lathe
Built with a Ø600 mm swing, Ø105 mm big-bore spindle, and up to 3,000 mm center distance for large shafts, oilfield pipes, and heavy drums.
- Travel / Max Swing
- Ø600 mm Swing · 1500–3000 mm
- Spindle Speed & Nose
- A2-11 · 1,600 RPM · Ø105 mm Bore
- Main Motor
- 11 / 15 kW
- Repeatability
- ±0.005 mm
Sales & Application Engineering
Send Your Inquiry
Complete the 3 fields below and our engineering team will respond promptly.