Induction-Hardened Box Ways vs. Preloaded Roller Linear Guides in CNC Machining
Modern cylindrical roller linear guides have bridged the rigidity gap with traditional box ways while delivering 3x faster rapid traverse and zero stick-slip micro-positioning.
WMT Mechanical Design Office
Guideway Tribology & Structural Stiffness Group
Key Engineering Takeaways
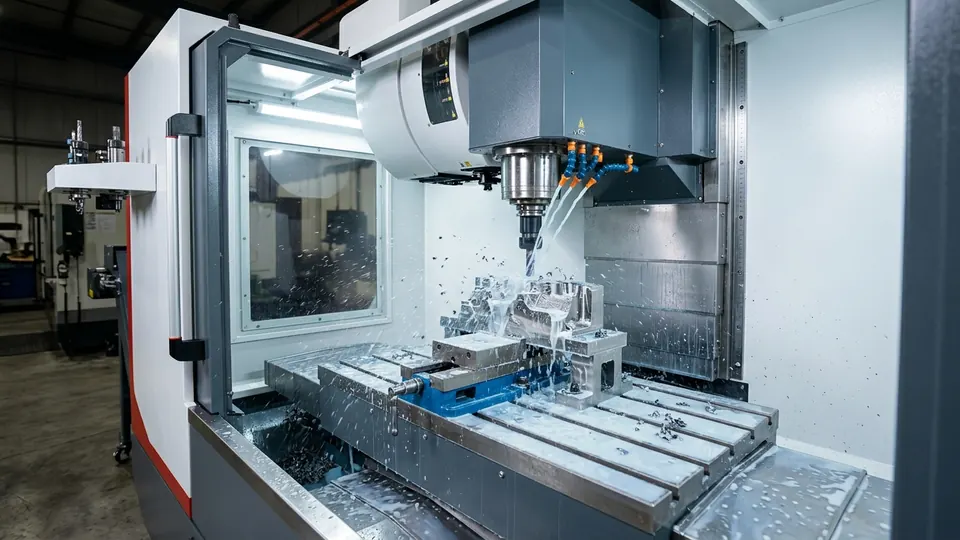
- —Cylindrical roller linear guides (used on WMT VMC and TCK series) replace point contact (ball guides) with line contact, boosting radial load capacity by 180%.
- —Induction-hardened box ways (HRC 52+) paired with hand-scraped Turcite-B (used on WMT CK series) provide hydro-dynamic oil film damping ideal for heavy interrupted turning.
- —For 3D high-speed mold surfacing and high-volume cycle work, preloaded roller guides eliminate quadrant glitch marks and reduce servo power draw by 40%.
1. Ball Linear Guides vs. Cylindrical Roller Linear Guides vs. Box Ways
Many machinists still associate "linear guides" with early-generation ball-bearing rails that lacked rigidity under heavy steel roughing. Modern WMT vertical machining centers (VMC650/850/855) and slant-bed turning centers (TCK50/52/56) do not use standard ball rails—they utilize heavy-duty cylindrical roller linear guideways.
Because a cylindrical roller contacts the hardened raceway along a continuous line rather than a microscopic sphere point, elastic deformation under shock loading drops dramatically while maintaining a low coefficient of friction (μ ≈ 0.003).
| Mechanical Property | Ball Linear Guide | WMT Cylindrical Roller Guide | WMT Hardened Box Way |
|---|---|---|---|
| Contact Geometry | Point Contact | Line Contact (Preloaded) | Surface Contact (Oil Film) |
| Friction Coefficient | 0.002 | 0.003 | 0.04 – 0.08 (Turcite-B) |
| Max Rapid Traverse | 36 – 48 m/min | 24 – 36 m/min | 8 – 15 m/min |
| Stick-Slip Behavior | Zero | Zero (Sub-micron response) | Present at ultra-low feeds |
| Vibration Damping | Low | High (with HT300 bed) | Maximum (Hydrodynamic) |
2. Matching Guideway Architecture to Your Part Mix
When contouring 3D mold surfaces or interpolating tight-tolerance bearing bores, any static-to-dynamic friction jump ("stick-slip") produces visible quadrant protrusions on the finished workpiece. Preloaded roller guides respond instantaneously to sub-micron servo encoder pulses, ensuring mirror-grade surface finishes.
Conversely, when turning forged steel shafts with heavy scale on a CK6150 or CK6160, the large surface area of induction-hardened box ways spreads impact energy across hundreds of square centimeters of cast iron.
- —Specify Size-45 cylindrical roller guides (standard on VMC855 and TCK56) when combining high-speed toolpaths with heavy roughing.
- —Specify induction-hardened box ways (standard on CK6140, CK6150, CK6160) for long-bed shaft turning and heavy interrupted OD cuts.
Related Machine Models
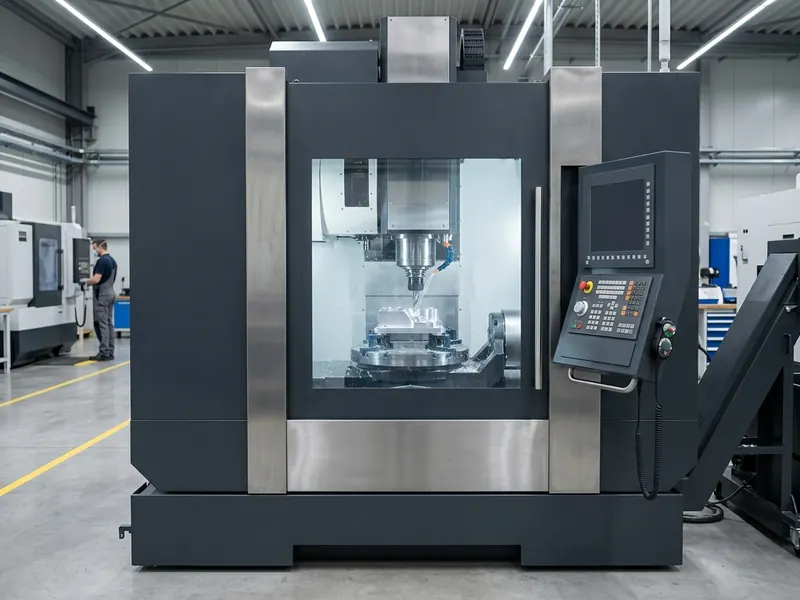
VMC855 Heavy-Duty Wide-Column Vertical Machining Center
Reinforced wide-span structural casting and 45 mm 3-axis roller linear guideways for aggressive steel roughing and deep mold cavities.
- Travel / Max Swing
- 855 × 550 × 550 mm
- Spindle Speed & Nose
- BT40 · 8,000 / 10,000 RPM
- Main Motor
- 15 / 18.5 kW
- Repeatability
- ±0.003 mm
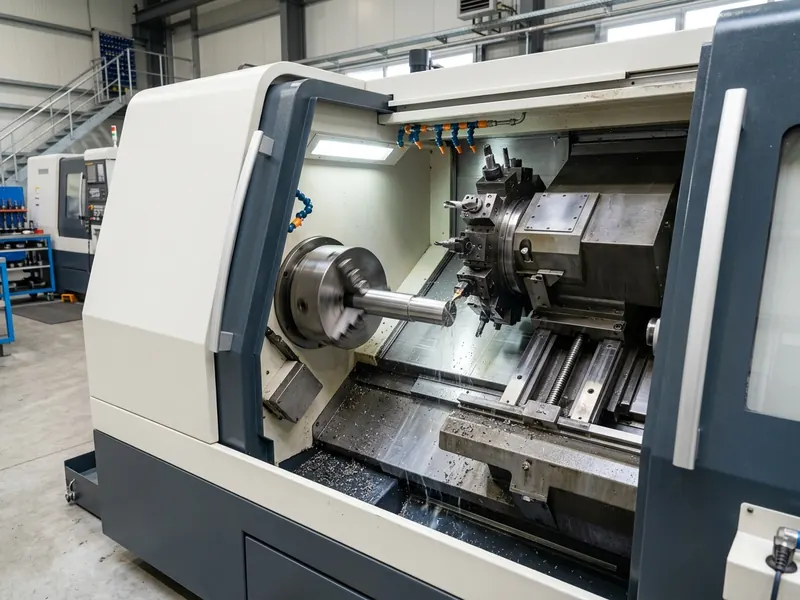
TCK56 Heavy-Duty 45° Slant Bed CNC Turning Center
Equipped with an A2-8 spindle nose, 10-inch hollow hydraulic chuck, Ø75 mm bar bore, and 15/18.5 kW drive for heavy alloy steel turning.
- Travel / Max Swing
- Ø560 mm Swing · 650 mm Length
- Spindle Speed & Nose
- A2-8 · 3,000 RPM · Ø75 mm Bore
- Main Motor
- 15 / 18.5 kW
- Repeatability
- ±0.003 mm
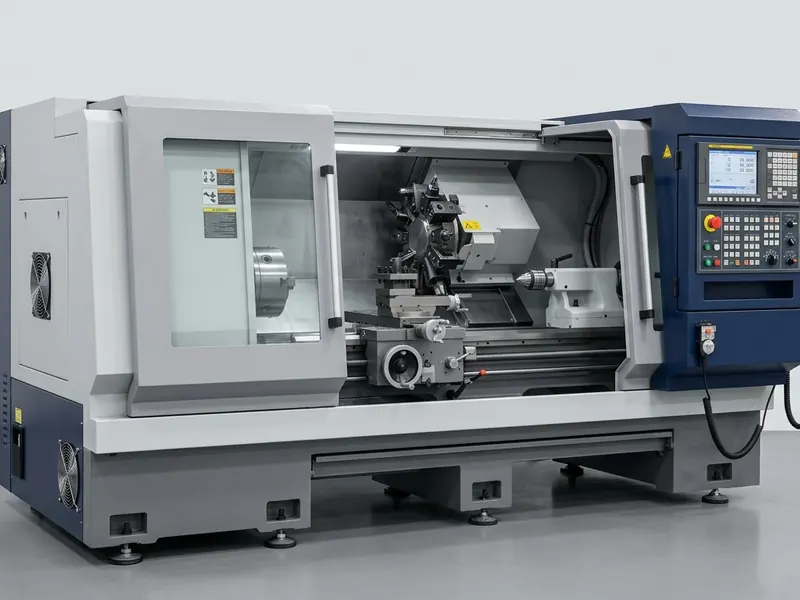
CK6150 Heavy-Duty Horizontal Flat Bed CNC Lathe
Wide 390 mm induction-hardened box ways and Ø82 mm big-bore spindle for long shafts, hydraulic cylinders, and medium-heavy flanges.
- Travel / Max Swing
- Ø500 mm Swing · 1000–2000 mm
- Spindle Speed & Nose
- A2-8 · 2,000 RPM · Ø82 mm Bore
- Main Motor
- 11 kW
- Repeatability
- ±0.005 mm
Sales & Application Engineering
Send Your Inquiry
Complete the 3 fields below and our engineering team will respond promptly.